
Tech
Who Manufactures PCB Assembly? – A Deep Dive into the Key Players and Processes


Printed Circuit Board (PCB) assembly is at the heart of every modern electronic device. Whether it’s your smartphone, computer, or even medical equipment, PCB assembly is essential for making these devices function. But have you ever wondered who manufactures PCB assembly? What’s involved in the process? Let’s look closer at the companies and technologies behind PCB assembly manufacturing.
What Is PCB Assembly (PCBA)?
Printed Circuit Board Assembly, commonly known as PCB assembly (PCBA), is the process that transforms a bare printed circuit board (PCB) into a fully functional electronic circuit. This involves mounting and soldering electronic components such as resistors, capacitors, diodes, and integrated circuits onto a PCB to enable it to perform its intended functions. The PCBA process is fundamental to all electronic devices, ensuring the electrical pathways required for components to communicate and work together.
In the early stages of electronics, assembling a PCB was a labor-intensive process that required human precision. Nowadays, with advancements in technology, the process is highly automated, increasing both speed and accuracy while minimizing the risk of human error. However, manual soldering and inspection still play a role in specific industries, particularly in cases where specialized or sensitive components are involved.
PCB assembly follows a structured process, with critical stages that include surface mounting and through-hole mounting. Surface Mount Technology (SMT) is the most common method, where components are placed directly onto the board’s surface using specialized machinery. SMT is ideal for compact, high-density assemblies, as it allows components to be mounted on both sides of the PCB.
Through-hole technology (THT), on the other hand, involves inserting components with leads through holes in the board and soldering them on the opposite side. THT is preferred for components that need mechanical solid support, such as connectors and transformers.
The PCBA process also includes soldering, where a solder paste is applied to the board to attach the components securely. This is followed by reflow soldering, which uses heat to melt the solder and permanently bond the components to the PCB. Afterward, the assembled board undergoes testing and inspection to ensure it functions as intended. Advanced techniques such as Automated Optical Inspection (AOI) and X-ray inspection help detect potential issues early, reducing the risk of faulty boards reaching the market.
Understanding how PCB assembly works is just the beginning. Next, let’s explore the different types of manufacturers involved in the PCBA process.
Types of PCB Assembly Manufacturers
PCB assembly is vast, and not all manufacturers operate under the same model. Depending on the scale and complexity of the project, different types of PCB assembly services manufacturers are available, each catering to specific needs and industries.
- Custom PCB Manufacturers
Custom PCB manufacturers are specialists who provide tailored solutions for industries with unique or highly complex requirements. These manufacturers typically serve sectors such as aerospace, automotive, medical devices, and defense, where precision and reliability are crucial.
Since they work on smaller-scale projects with more intricate designs, they offer greater flexibility in production, allowing businesses to experiment with new designs or prototype custom products. This is particularly valuable for companies that must produce limited boards for testing or niche applications.
- Mass Production PCB Manufacturers
In contrast, mass production manufacturers focus on high-volume output, typically serving consumer electronics and automotive industries. These manufacturers are designed to handle large quantities of PCBs quickly and efficiently, relying heavily on automation to meet tight deadlines.
Mass production PCB manufacturers are best suited for businesses that need thousands or millions of PCBs for their products, such as smartphones, televisions, and other consumer goods. While they may not offer the same level of customization, their ability to deliver at scale makes them indispensable for companies with large production runs.
- Contract Electronics Manufacturers (CEMs)
Contract Electronics Manufacturers (CEMs) provide end-to-end services, making them a popular choice for businesses that want to outsource the entire PCB manufacturing process. CEMs handle everything from design and prototyping to assembly and testing. They are flexible in project size, offering services for small and large production runs.
What sets CEMs apart is their ability to manage the entire production lifecycle, which can be particularly advantageous for startups and mid-sized companies that lack the in-house expertise or infrastructure to manage PCB assembly. By partnering with a CEM, companies can focus on their core competencies while leaving the technical aspects of PCB assembly to the experts.
Now that we’ve explored the different types of PCB assembly manufacturers let’s examine some of the major players in the global market.
Top PCB Assembly Manufacturers Around the World
The global PCB assembly industry is vast. Research and Markets report that “the global PCB market size is projected to reach $86.17 billion by 2026, at a CAGR of 3.3% from 2021, driven by the increasing demand for automotive electronics, smartphones, and the ongoing rollout of 5G technology.”
Several key players are leading the charge in different regions and sectors. These companies produce the PCBs that power everything from consumer electronics to critical medical devices and aerospace technology. Below are some top PCB assembly manufacturers and PCB assembly services suppliers known for their expertise, scale, and innovation.
- Foxconn
Foxconn, a Taiwanese multinational electronics manufacturer, is arguably the biggest name in PCB assembly. Known for producing electronic devices for global giants like Apple, Foxconn handles large-scale PCB assembly for smartphones, tablets, and other consumer electronics.
With factories across the globe, including in China and the United States, Foxconn’s massive production capacity allows it to meet the high demands of the tech industry. Despite being a mass-production powerhouse, Foxconn maintains stringent quality control, ensuring each PCB functions reliably.
- Jabil
Jabil is a U.S.-based company that provides comprehensive PCB assembly services. Its expertise spans various industries, including aerospace, defense, and healthcare, where precision and reliability are paramount.
Jabil stands out for its ability to handle custom and mass-production PCB assembly, making it a versatile player in the global market. The company focuses on delivering high-quality PCBs while adhering to strict regulatory standards, particularly in industries where the slightest error could have serious consequences.
- TTM Technologies
TTM Technologies, headquartered in the U.S., specializes in producing high-end aerospace, defense, and communications PCBs. Known for handling complex, multilayer PCBs, TTM Technologies excels in projects that require high precision and advanced engineering capabilities. TTM’s strong engineering teams work closely with clients to ensure that each PCB design meets the specifications needed for critical applications.
- Flex Ltd.
Flex Ltd., formerly Flextronics, is a global manufacturer known for flexibility and innovation. Flex serves various industries, including automotive, consumer electronics, and healthcare, by providing mass production and custom solutions. The company emphasizes sustainable manufacturing practices, making it a leader in environmentally conscious PCB assembly. Flex’s ability to adapt to various industries while maintaining high production quality makes it a top choice for businesses worldwide.
Having explored some of the top manufacturers, it’s time to break down the detailed steps involved in PCB assembly from start to finish.
The PCB Assembly Process: From Concept to Completion
PCB assembly is a complex, multi-stage process that transforms a blank PCB into a fully functioning circuit board. Whether for a prototype or a mass-produced product, the steps involved in PCB assembly require precision, efficiency, and careful attention to detail.
- Design and Prototyping
The design and prototyping stage is crucial before the actual assembly begins. Manufacturers work closely with clients to develop the PCB layout based on the product’s technical requirements. The design phase involves creating detailed schematics and ensuring the placement of each component on the board is optimized for performance.
Prototyping allows the manufacturer to develop an initial sample of the PCB, which can be tested for functionality and design flaws. This stage is vital for identifying any potential issues before full-scale production begins.
- Component Sourcing
Once the design is finalized, manufacturers source the necessary electronic components for the assembly. Component sourcing is an essential step, as the quality of the components directly affects the reliability and performance of the final product.
Manufacturers often rely on a network of trusted suppliers to obtain components like resistors, capacitors, ICs, and connectors. Timely sourcing is critical to keeping production schedules on track, particularly for large-scale manufacturing projects.
- Surface Mount Technology (SMT)
SMT is the backbone of modern PCB assembly. In this step, components are mounted directly onto the surface of the PCB using automated machines. A solder paste is applied to the board, and pick-and-place machines position each component with high precision.
Once the components are in place, the board passes through a reflow oven, where heat is applied to melt the solder paste and secure the components in place. SMT is the most efficient method for assembling high-density PCBs, making it ideal for compact devices like smartphones and wearables.
- Soldering and Inspection
After the SMT process, the PCB is inspected to ensure all components are correctly placed and securely soldered. This step includes visual inspections and advanced techniques like Automated Optical Inspection (AOI) and X-ray scanning.
These systems can detect any soldering defects or misplaced components. If any issues are found, the board is sent back for rework. Manual soldering may still be required for through-hole components, particularly for connectors and other components that cannot be surface-mounted.
- Testing and Quality Assurance
The final stage of PCB assembly involves rigorous testing to ensure the board functions as intended. Electrical tests check for shorts, open circuits, and signal integrity. Functional testing ensures the board can perform its designated tasks without errors. Quality assurance teams conduct additional inspections to ensure the product meets all industry standards and client specifications before it’s packaged and shipped.
Innovations in PCB Assembly Technology
PCB assembly continues to evolve rapidly. According to Statista, the global PCB market was valued at approximately $63.5 billion in 2021 and is expected to grow significantly due to increasing demand for electronic devices across various sectors, including automotive, healthcare, and consumer electronics, and driven by consumer demands for faster, smaller, and more efficient electronics. As a result, manufacturers are adopting cutting-edge technologies and methods to remain competitive and meet the growing needs of industries like telecommunications, medical devices, and consumer electronics. Let’s explore some key innovations that are reshaping PCB assembly.
- Automation and Artificial Intelligence (AI)
Automation has revolutionized the PCB assembly process, speeding up production while reducing human error. Modern PCB assembly lines utilize robotic arms and machines to handle intricate components and complex designs with high precision.
AI is taking automation further by integrating machine learning into these processes. AI-powered machines can learn from production data to optimize placement accuracy and minimize defects. This innovation has reduced production times and improved quality, particularly for complex, multilayer boards used in advanced electronics.
- Advanced Materials and Eco-Friendly Solutions
As the world moves towards sustainability, PCB manufacturers are not far behind. One of the most significant innovations is using advanced materials such as flexible substrates, which allow PCBs to be designed in compact, lightweight forms.
These flexible PCBs are ideal for modern devices like smartphones, wearable tech, and medical implants that require compact, bendable designs. Alongside flexible materials, manufacturers are exploring biodegradable PCBs made from eco-friendly compounds, making electronics more sustainable. This shift toward greener solutions is essential as companies worldwide strive to reduce electronic waste.
- Miniaturization and Enhanced Efficiency
Miniaturization is a vital trend in the race to build smaller and more powerful devices. Micro-PCBs are now used in IoT devices, drones, and advanced medical devices, packing more components into smaller spaces without sacrificing performance.
trend of shrinking electronics, driven by consumer demands for portability and convenience, pushes PCB manufacturers to refine assembly techniques further. Combining high component density with efficiency improvements ensures manufacturers can meet the requirements of next-gen electronics without increasing production costs.
While these innovations drive PCB assembly forward, choosing the right partner is just as important. Let’s explore critical factors in selecting a PCB assembly manufacturer.
Key Factors in Choosing a PCB Assembly Manufacturer
Choosing the proper PCB assembly manufacturer is not just about finding someone to produce your designs. It’s about finding a partner that understands your specific needs and can ensure quality, reliability, and scalability. Here are the most critical factors when selecting a PCB assembly supplier.
- Experience and Industry Expertise
One of the first things to consider is the manufacturer’s experience. PCB assembly requires a deep understanding of various industries, such as aerospace, medical devices, automotive, and telecommunications. Each industry has its own set of requirements, and an experienced manufacturer can guide you through design optimization, component selection, and compliance with industry standards. Their knowledge can help you avoid common pitfalls, such as design errors or delays in the production process.
- Certifications and Quality Standards
Ensuring quality is paramount when choosing a PCB assembly supplier. Manufacturers should adhere to internationally recognized quality standards like ISO 9001 or IPC-A-610. These certifications guarantee that the manufacturer follows strict guidelines and practices during production. Additionally, RoHS compliance is essential for environmental sustainability, particularly for companies concerned with hazardous materials in electronics. Working with a certified manufacturer can give you peace of mind that your products will be safe, reliable, and compliant with industry regulations.
- Scalability and Production Capacity
Whether starting with a small prototype or planning to scale into mass production, choosing a manufacturer who can grow with your needs is essential. A good partner should be able to handle everything from low-volume prototype runs to large-scale production without compromising on quality. Scalability is critical for businesses anticipating growth, as it saves time and effort that would otherwise be spent switching manufacturers as your production volume increases. Ensure the PCB assembly house has the equipment, workforce, and logistical capacity to meet your short-term and long-term goals.
Now that you know what to look for in a PCB assembly partner, it’s time to consider the future. Today’s trends shaping the PCB industry will be critical to your approach to your next project.
Future Trends in PCB Assembly Manufacturing
The PCB assembly industry is continuously evolving, and keeping an eye on future trends can give you a competitive edge. These trends shape how PCBs are manufactured and influence how industries like electronics, healthcare, and automotive operate. Grand View Research highlights that the global PCB market is projected to grow at a compound annual growth rate (CAGR) of 5.3% from 2022 to 2030, driven by technological innovations such as AI and 5G, which require more sophisticated PCB assemblies.
Let’s examine some key trends that will dominate the PCB assembly market in the coming years.
- Industry 4.0 and Smart Manufacturing
Industry 4.0, which refers to the current automation and data exchange trend in manufacturing technologies, is transforming PCB assembly. Smart factories equipped with sensors, IoT devices, and AI-driven automation allow PCB manufacturers to enhance productivity and efficiency.
This move towards data-driven processes enables real-time monitoring of production lines, predictive maintenance, and more informed decision-making. In intelligent manufacturing environments, machine-to-machine communication allows for greater flexibility in adapting to changes, reducing downtime, and optimizing assembly lines.
- On-Demand Manufacturing and Customization
With consumer demands for personalized electronics on the rise, PCB manufacturers are increasingly adopting on-demand manufacturing practices. Using advanced technologies like 3D printing and digital manufacturing, manufacturers can now offer rapid prototyping and customization for smaller production runs.
This is particularly valuable for startups and innovators who require custom solutions but don’t have the budget or need for mass production. On-demand PCB assembly services provide flexibility and faster turnaround times, which is crucial for companies looking to get their products to market quickly.
- Global Supply Chain Adaptations
The COVID-19 pandemic has exposed vulnerabilities in global supply chains, and the PCB assembly industry has not been immune. As companies faced component shortages and shipping delays, manufacturers have adapted by reshoring production or diversifying their supply chains. We expect to see more localized production hubs, particularly in regions with solid technology sectors. This shift toward shorter, more resilient supply chains ensures that manufacturers can meet demand despite global disruptions. Additionally, companies are investing in better inventory management systems to avoid disruptions caused by shortages.
As these trends continue to shape the future of PCB assembly manufacturing, staying informed will help you make the best decisions for your projects and business.
How PCB Assembly Powers Various Industries
PCB assembly is vital across numerous sectors, providing the precision, efficiency, and versatility needed to drive technological innovation. From the devices we use daily to critical systems in healthcare and defense, PCBs are the backbone of modern technology.
- Consumer Electronics
Consumer electronics is one of the most visible sectors that are reliant on PCB assembly. Devices like smartphones, tablets, and gaming consoles depend on the intricate circuits that PCBs provide. Consumers demand faster, smaller, and more powerful devices, so manufacturers like Foxconn and Flex Ltd. work tirelessly to produce miniaturized PCBs with enhanced designs. These innovations meet the need for high performance in compact products.
- Automotive Industry
In the automotive industry, the rise of electric vehicles (EVs) and advanced driver-assistance systems (ADAS) has revolutionized the role of PCBs. PCBs are used in everything from engine control units to in-car entertainment systems, supporting modern vehicles’ numerous sensors and electronic components. Manufacturers like TTM Technologies and Jabil produce PCBs that meet this fast-evolving sector’s stringent quality and safety standards.
- Aerospace and Defense
The aerospace and defense sectors rely on PCBs, from military drones to satellite systems, for critical applications. These industries demand flawless performance under extreme conditions, requiring highly specialized PCBs that are durable, reliable, and resistant to harsh environments. Custom PCB manufacturers provide tailored solutions to meet these high-stakes needs, where performance and quality are crucial to national security.
- Healthcare and Medical Devices
Medical devices such as pacemakers, MRI machines, and ventilators depend heavily on PCBs to function effectively. Precision and reliability are paramount in healthcare, as any failure could have life-threatening consequences. The trend towards miniaturization is especially relevant here, with wearable medical devices requiring compact, dependable PCBs to deliver optimal patient care.
- Telecommunications
Telecommunications relies on flex pcb for everything from cell towers to mobile devices. As 5G technology rolls out globally, there is an increasing demand for PCBs that can handle high-frequency signals and ensure stable communication. The need for advanced PCB assembly solutions will grow as this sector expands.
The Backbone of Modern Technology
Finding the right PCB assembly services supplier is more than just ticking boxes on a checklist—it’s about building a partnership that supports your vision. A dependable PCB assembly manufacturer ensures your designs translate seamlessly into functional, high-quality products. With the right PCB assembly supplier, you’ll avoid production headaches and missed deadlines, allowing more time to innovate.
Whether it’s quick turnarounds or custom solutions, a reliable PCB assembly factory will understand your unique challenges and deliver on time. Ready to elevate your next project? Connect with the right supplier and watch your electronics soar.
Since January 1, 2026, structured electronic invoicing has become mandatory for almost all transactions between Belgian VAT-registered businesses. These invoices are exchanged through the Peppol network instead of with traditional PDF-based processes. For businesses, the decision on the provider can have a lot to do with what’s the destination of the invoice than it does with the transaction itself. Integration, inbound processing, validation, monitoring, security, and support can all be key factors to how well e-Invoicing integrates into everyday finance operations. An easy way to evaluate a Peppol access point Belgium solution is to see what happens before, during, and after an invoice moves through the network.
- ERP and accounting integration.
The first question would be how well the Access Point is integrated into the existing systems used by the business. An enterprise can generate invoices from an ERP, billing application, or multiple systems of different subsidiaries in different companies. The Access Point needs to have the invoice information without creating an extra manual process for each system and how that invoice data needs to be sent to the Access Point. This means not just a simple integration statement. Businesses should know which APIs, connectors, and formats are available and how data is mapped and whether invoice status can be sent back to the ERP. In a large organization, the integration model should also be flexible for future change. Another legal entity or ERP should not need to be added to the overall e-Invoicing system.
- Stronger support for Sending and receiving.
A common mistake is to evaluate a provider on outbound invoicing. Belgian businesses need to be able to receive structured electronic invoices from their suppliers. Businesses should adapt their systems to receive structured invoices, for example, those that mainly invoice private individuals, the Belgian authorities say.
So, both directions should benefit from the Access Point. For incoming invoices, companies should assess where documents are led in accounting or ERP, whether supplier information can be matched automatically, and how exceptions are handled if an invoice can’t be processed.
- Invoice Validations before the Invoice Is Processed in the Network.
An efficient Access Point cannot be thought of as just a delivery mechanism. Data on the invoice needs to be structured according to the proper business and structure and business rules in order to be processed properly. Validation makes it possible to identify missing and inaccurate data before the invoice is sent.
This is particularly useful for the organizations that receive their invoices from different sources. If data is created using different systems, validation is most important so that there are no mistakes. The vendor should be able to provide an explanation of the types of validations in place, the location of those validations, and the outcome of those validations that are not successful.
- Visibility Into Invoice Status and Exceptions.
Once an invoice has been sent, finance teams need to know what happened to it. A Belgium e-invoicing solution should have clear visibility into transaction status, delivery, and errors in Belgium. Ideally, this information should flow back into the enterprise’s current finance workflow rather than being stuffed away in a provider dashboard. Particularly when invoice volumes are high. A finance team should be able to determine which invoices got processed and which ones should be paid attention to and why the transaction failed at the end of the month. Searching, filtering, and reporting on these events can also facilitate month-end reconciliation as well.
- Scalability across entities and Invoice volumes.
An Access Point that works for one legal entity may not necessarily be appropriate for a multinational with multiple Belgian entities. Enterprises should look into transaction volumes, number of entities, ERP environment, and suppliers and customer relationships before choosing a provider. They should know how onboarding works when a new entity enters the network. Will it also need an implementation in a new system? Can multiple entities be managed centrally? How do Peppol identifiers get handled? These questions help to determine whether a Belgium Peppol Access Point can be part of the organization’s operating model and not just its invoice volume.
- Provider Support and Long-Term Operations.
What happens after implementation is the last step. A certified Peppol provider Belgium should be able to support the enterprise when integrations change, transaction failures occur, or new requirements impact the invoicing process. Before the contract is signed, the support arrangements should be in place. Enterprises should know the response time, escalation procedure, maintenance window, and responsibilities if there is an ERP, Access Point, or recipient issue. It is also worth checking if the provider can support monitoring and reporting without having finance teams lean on technical experts completely.
What Should Enterprises consider When Comparing?
Enterprises should not just choose providers based on network connectivity alone and compare them in terms of their network compatibility. They may rather compare on the following points: • Integration with ERP and accounting
• Sending and receiving features
• Invoice verification
• Status and exceptions handling
• Multi-company
• Security and business continuity
• Support and service management.
A company with one accounting system and few invoices may prefer something less complicated. An enterprise with multiple ERP systems will generally need more sophisticated integration and monitoring.
The Belgian authorities are careful to distinguish between end-user software and service providers providing the services to Peppol. Companies that have this software and can choose their own Access Point are referred to as certified service providers.
The Right Access Point Should Fit the Entire Invoice Process.
The purpose in choosing a Belgium e-Invoicing service provider was not to connect the company with Peppol. The service provider will be a part of the whole system through which invoices have to be sent, received, and tracked.
So Peppol Belgium readiness is as much an operational issue as it is a compliance issue. The company could put even more pressure on Finance if the service provider is a good partner for connectivity but not good at tracking failure. To the contrary, a solution that works well with one ERP but does not work well for multi-entity processes will soon start to look restrictive as the business grows.
So for an enterprise that is considering Peppol access point Belgium service, the right assessment always starts with the invoice process. How is the invoice created? How is it sent to the Access Point? Are there any validations prior to sending it out? How is it received by the recipient? What happens in case of failure? Can Finance trace the problem without having to follow another manual process? These considerations will help us choose an Access Point for enterprise e-Invoicing that works well.
Best Managed IT Services Companies for Proactive IT Support
IT issues don’t usually come up at an opportune time either; the failure of servers, security threats, or network slowdowns can disrupt business operations and cause delays that can end up being costly. That is why a number of companies turn to managed IT services with their emphasis on prevention rather than reaction.
The best managed IT service providers have all of the following capabilities: monitoring, automation, cybersecurity, maintenance, and technical skills. In addition, the proper provider is able to tailor its preventative strategy to fit the size of the company.
Best Managed IT Services Companies for Proactive Support
For firms considering IT management services, a more proactive approach is required than just basic help desk services. Proactive service involves monitoring systems and taking care of issues even before they turn into major problems.
1. Longi Engineering
Longi Enginuity Technologies is a strong choice for businesses seeking proactive managed IT support. Its approach focuses on maintaining reliable technology through continuous oversight, cybersecurity, technical support, and preventive IT management.
Proactive managed services ensure that any technical issues are detected prior to creating any disruptions. The process includes maintenance, security, and troubleshooting of the network to prevent any downtime.
2. IBM Managed Services
IBM Managed Services is highly suitable for large organizations with highly complicated IT setups. These include its strong points, such as hybrid cloud management, artificial intelligence, and IT operations at the enterprise level.
One of the greatest benefits is the analysis of infrastructure information by means of AIOps, which helps recognize possible problems that could affect the performance of IT infrastructures.
3. Accenture Managed Services
Accenture offers managed IT services along with cloud management, digital transformation, and cybersecurity. This comprehensive service offering makes Accenture a suitable choice for firms that deal with a complex IT landscape.
A proactive strategy offered by Accenture includes infrastructure monitoring, security analysis, and compliance management. This will help companies to uncover any potential problems that may affect their operations.
4. HCLTech
HCLTech offers managed infrastructure services, service desk support, automation, and hybrid workplace management. Its approach is particularly relevant for organizations that want routine IT tasks handled consistently.
The DRYiCE automation solution can facilitate automated maintenance and automated incident management. These processes will reduce the need for manual effort while resolving all the problems even before they arise.
5. Tata Consultancy Services
Tata Consultancy Services provides managed infrastructure and cloud services for large organizations operating at significant scale. Its services emphasize automation, monitoring, and efficient enterprise IT management.
TCS uses its Ignio AIOps platform to detect unusual system behavior and identify potential issues. Its automation capabilities can also support faster resolution and more consistent infrastructure performance.
Strong Managed IT Providers for Growing Businesses
Enterprise providers are not the only options for proactive IT support. Mid-market and growing businesses often need providers that combine continuous monitoring with responsive service, security, and practical IT management. Managed IT Services Connecticut represents this type of ongoing support, where businesses can rely on managed technology oversight instead of handling every IT issue internally.
6. Ntiva
Ntiva provides managed IT services, cybersecurity, compliance, and IT strategy. The company’s solutions are suitable for firms that require consistent supervision while not keeping all IT services within their walls.
Continuous monitoring helps in identifying technical and security issues early on. Also, because it is compliance-based, it is an ideal choice for firms that have to abide by certain regulatory standards.
7. Dataprise
Dataprise provides managed IT, cloud, infrastructure, and cybersecurity services for mid-market firms. The approach entails ensuring there is visibility within the technological environment of the business and finding any weaknesses that may exist.
Network assessment and threat hunting help in the proactive management of risks. Through this service, businesses will be able to manage any infrastructure or cybersecurity challenges proactively.
8. Thrive
Thrive provides managed IT services with a focus on cloud environments, cybersecurity, infrastructure, and digital transformation. Its services are suited to growing businesses managing increasingly complex technology systems.
Continuous application and network monitoring can help identify performance concerns early. Its hybrid cloud capabilities also support organizations moving between traditional infrastructure and cloud-based environments.
What Makes a Managed IT Provider Proactive?
The choice of a managed IT services company is not just about the comparison of its services. A true proactive vendor has an infrastructure set up in such a way that any issues can be detected and solved before downtime occurs. Connecticut managed IT services adhere to this philosophy by concentrating on management and not on technical problems.
Continuous Monitoring
A good provider will continuously monitor their networks, servers, endpoints, applications, and other systems. Notifications allow their technical staff to investigate any suspicious behavior and prevent it from becoming a bigger problem.
Automated Maintenance
Regular patching, updates, system checks, and routine maintenance reduce preventable technology problems. Automation helps these tasks happen consistently without depending entirely on manual intervention.
Integrated Cybersecurity
Preventive IT support is also crucial to handling security threats. Threat management, endpoint security, vulnerability management, and access control all play a role in minimizing the risk of turning a security threat into a breach.
Predictive IT Management
Sophisticated service providers employ analytical tools and automation to uncover trends that point towards future failure. Through this, IT departments can take action based on trends rather than user complaints.
Choosing the Right Provider for Proactive IT Support
The appropriate provider will be determined by the technology environment within the organization, the size of the organization, its security needs, and its business objectives. In some cases, the large corporation may need a provider that has hybrid cloud capabilities along with automation capabilities, whereas other organizations may need only a focused managed service partner.
Another criterion that an organization must consider when selecting an appropriate provider is that of processes and measurable performance standards for service delivery.
Building a More Proactive IT Environment
Proactive IT support is ultimately about preventing avoidable disruption. The strongest managed IT services companies continuously monitor technology, automate routine maintenance, strengthen security, and use data to identify emerging problems.
Selecting a provider with these capabilities creates a more structured approach to IT management. Longi Enginuity Technologies can support this proactive model through managed IT services designed around business technology needs. The right partnership helps turn IT from a source of unexpected problems into a stable foundation for daily operations.
Tech
Machine Safety Services and Control System Integration: Building Safer, Smarter Industrial Operations

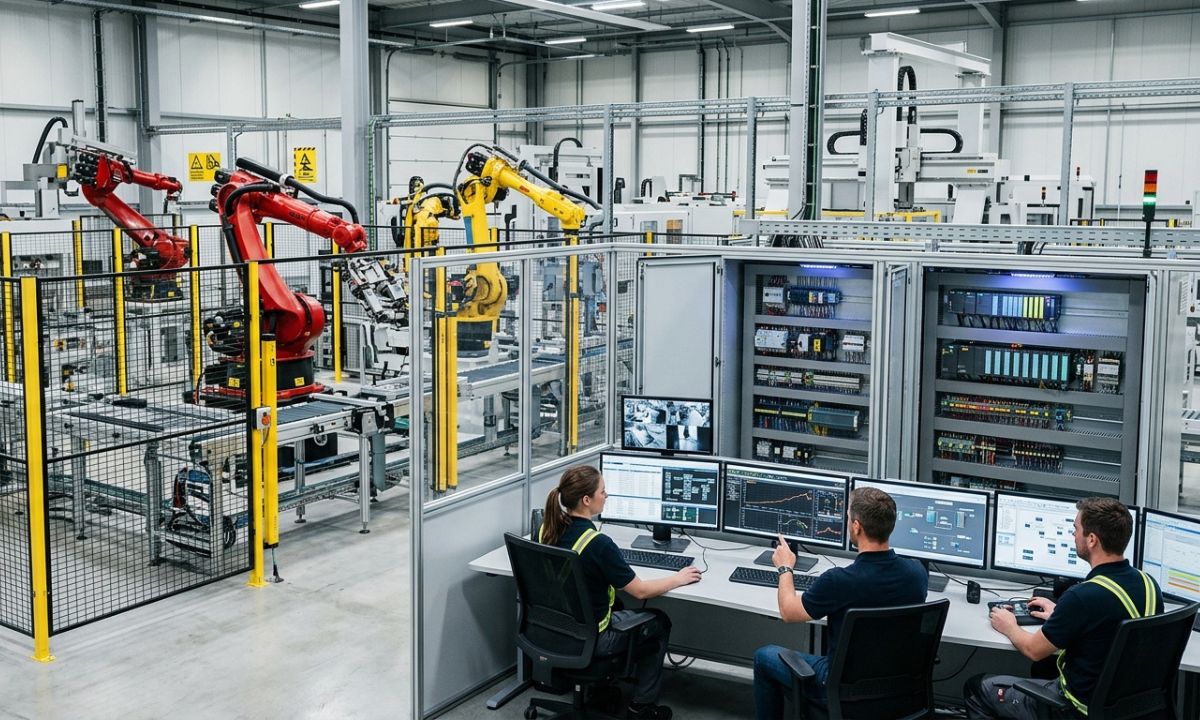
A production line can run thousands of cycles in a day without a problem. Then one small control failure, an outdated safety circuit, or a poorly integrated machine creates a serious interruption.
That is why modern industrial automation is no longer just about making equipment run faster. It is about making systems work together safely, reliably, and intelligently.
This is where machine safety services and control system integration become particularly important. Manufacturers and other industrial operators need more than individual machines with sophisticated controls. They need those machines, safety devices, sensors, software, and production systems to communicate effectively.
A well-designed automation system can improve productivity while also helping reduce operational risk, improve product consistency, modernize aging equipment, and give plant managers better visibility into what is happening on the production floor.
For companies dealing with legacy controls or increasingly complex production requirements, that combination can make a substantial difference.
Table of Contents
- What Are Machine Safety Services?
- Understanding Control System Integration
- Why Machine Safety and Automation Go Together
- Common Problems With Legacy Control Systems
- What a Control System Integrator Actually Does
- Key Benefits of Modern Automation Integration
- Machine Safety Services vs. Traditional Safety Upgrades
- How Pacific Blue Engineering Supports Industrial Automation
- Industries That Can Benefit From Control Integration
- Questions to Ask Before Starting an Automation Project
- Frequently Asked Questions
- Final Thoughts
What Are Machine Safety Services?
Machine safety services are engineering and technical services designed to identify and reduce hazards associated with industrial machinery and automated processes.
These services can involve reviewing existing equipment, identifying potential hazards, evaluating safety controls, and helping businesses implement appropriate protective measures.
Depending on the application, machine safety work may include:
- Safety risk assessments
- Machine guarding evaluation
- Safety circuit design
- Emergency stop systems
- Safety PLC implementation
- Interlocking systems
- Presence sensing devices
- Light curtains and safety scanners
- Safety relay systems
- Control system validation
- Safety documentation
- Machine modernization
The important point is that machine safety isn’t simply about adding an emergency-stop button and calling the job finished.
A machine may be technically functional while still having weaknesses in its safety architecture. For example, an outdated control panel may not communicate properly with newer safety devices. A modified production line may introduce hazards that weren’t present when the original machine was installed.
That’s why safety needs to be considered as part of the complete automation system.
Understanding Control System Integration
Control system integration involves bringing different automation components together so they operate as one coordinated system.
Think about a modern production facility. It may contain programmable logic controllers, variable frequency drives, robots, sensors, HMIs, industrial networks, safety systems, databases, and supervisory software.
If each component works independently, operators may spend unnecessary time troubleshooting problems and collecting information manually.
An experienced control system integrator connects these technologies and develops the control architecture needed for the application.
A typical integration project might include:
- Reviewing the existing process
- Identifying operational requirements
- Developing the control architecture
- Selecting suitable automation hardware
- Programming PLCs and HMIs
- Integrating sensors and field devices
- Connecting safety systems
- Establishing industrial communications
- Testing the system
- Commissioning the equipment
- Training operators and maintenance personnel
The goal isn’t simply to install new technology. The goal is to create a system that solves an actual operational problem.
Why Machine Safety and Automation Go Together
Safety and productivity are sometimes treated as separate objectives. In practice, they often overlap.
Consider a machine that frequently stops because operators have to manually intervene. If the safety and control architecture is poorly designed, diagnosing those stops can become difficult.
A modern integrated system can provide clearer information about what happened and why.
For instance, instead of simply showing that a machine stopped, an HMI might identify a particular safety device, interlock, sensor, or process condition that triggered the shutdown.
That information can shorten troubleshooting time.
It can also help maintenance teams identify recurring issues before they turn into larger production problems.
Honestly, this isn’t talked about enough: good safety engineering can contribute to better operational visibility, not just compliance.
Common Problems With Legacy Control Systems
Many industrial facilities are still operating equipment that was installed years or even decades ago.
There’s nothing inherently wrong with keeping reliable equipment in service. The problem begins when the control technology becomes difficult to maintain or integrate.
Common warning signs include:
Obsolete PLC Hardware
Older PLCs and processors may no longer be supported by their manufacturers. Replacement components can become expensive or difficult to locate.
Limited Data Visibility
Some older systems provide very little useful production data. Operators may know that something went wrong but have limited information about the cause.
Difficult Troubleshooting
Legacy systems may rely heavily on undocumented wiring, outdated programming practices, or components that newer technicians aren’t familiar with.
Inconsistent Safety Architecture
Equipment modifications performed over the years can leave safety systems fragmented or difficult to evaluate as a whole.
Poor Communication Between Machines
Older equipment may not communicate easily with modern manufacturing software, plant networks, or newer automation platforms.
Replacing an entire machine isn’t always the answer.
In many situations, control system modernization can extend the useful life of existing equipment while bringing its controls closer to modern operational standards.
What a Control System Integrator Actually Does
A control system integrator sits between the business problem and the technology used to solve it.
That distinction matters.
A good integrator doesn’t start with, “Which PLC should we install?” The better question is, “What does this process need to accomplish?”
From there, engineers can determine the appropriate hardware, software, networking, safety architecture, and user interface.
An experienced integrator may work on projects involving:
- PLC programming
- HMI development
- SCADA systems
- Industrial networking
- Robotics integration
- Motion control
- Variable frequency drives
- Safety PLCs
- Electrical control panels
- Data collection
- Process automation
- Legacy system modernization
- System commissioning
This approach becomes especially useful when a project involves multiple vendors or generations of equipment.
Someone has to make all those pieces work together.
Key Benefits of Modern Automation Integration
A properly planned automation project can affect much more than machine speed.
Improved Machine Safety
Modern safety systems can help identify hazards and provide controlled responses when unsafe conditions occur.
Better Product Quality
Automation can reduce process variation by controlling important parameters consistently.
Reduced Downtime
When control systems provide better diagnostic information, maintenance teams can often identify problems faster.
Lower Operational Risk
Replacing unsupported components and improving system architecture can reduce some risks associated with aging equipment.
Better Production Data
Integrated systems can collect valuable information about machine status, production rates, faults, energy use, and other operational factors.
Easier Maintenance
Clearer programming, documentation, interfaces, and diagnostics can make systems easier for maintenance teams to understand.
Longer Equipment Life
Modernizing controls may allow an otherwise useful machine to remain productive without replacing the entire mechanical system.
Better Decision-Making
Plant managers can make more informed decisions when reliable production information is available instead of relying entirely on manual observations.
Machine Safety Services vs. Traditional Safety Upgrades
| Traditional Approach | Integrated Machine Safety Approach |
|---|---|
| Focuses mainly on individual safety devices | Considers the complete machine and control architecture |
| Often reactive | Can be based on systematic risk assessment |
| Limited diagnostic information | Better fault and status visibility |
| May rely heavily on standalone components | Can integrate safety PLCs and control systems |
| May address one machine at a time | Can consider connected production processes |
| Documentation may be limited | Documentation and validation can be built into the project |
This doesn’t mean every facility needs the most sophisticated safety technology available.
Quite the opposite.
The right solution depends on the machine, process, hazards, operating environment, and business requirements.
How Pacific Blue Engineering Supports Industrial Automation
Pacific Blue Engineering is an example of an engineering company focused on control system integration and industrial automation.
Its work covers tailored automation solutions designed around the specific requirements of industrial operations rather than forcing every customer into the same technology package.
That distinction is important because no two production environments are exactly alike.
A manufacturing plant may need to modernize legacy controls while maintaining existing equipment. A food and beverage operation may have different process, sanitation, and production requirements. A life sciences facility can have its own demanding automation and documentation considerations.
Pacific Blue Engineering provides control system integration services across industries including manufacturing, food and beverage, life sciences, entertainment, and transportation.
Its engineering approach can help businesses address several common industrial challenges, including:
- Modernizing legacy control systems
- Improving machine safety
- Optimizing production processes
- Enhancing product quality
- Reducing operational risk
- Integrating automation technologies
- Improving access to operational information
The value of this type of engineering work isn’t limited to the initial installation.
A well-designed system should also make sense five or ten years later when someone needs to troubleshoot a sensor, modify a process, replace a component, or understand why a machine stopped.
That’s where thoughtful systems engineering earns its keep.
Industries That Can Benefit From Control Integration
Manufacturing
Manufacturers often need to balance throughput, quality, safety, and equipment availability. Integrated controls can help coordinate machines and provide better information about production performance.
Food and Beverage
Food and beverage facilities depend heavily on consistent processes. Automation can help control production parameters while improving visibility into equipment and process conditions.
Life Sciences
Life sciences operations can involve complex processes where consistency, traceability, and reliable automation are particularly important.
Entertainment
Entertainment facilities can use sophisticated automation and control systems for equipment, attractions, specialized machinery, and operational processes.
Transportation
Transportation environments may involve complex mechanical and electrical systems that require reliable monitoring, control, and integration.
The technologies differ between these industries, but the underlying principle remains similar: connect the right systems and make them work together reliably.
Questions to Ask Before Starting an Automation Project
Before selecting an integrator or beginning a major controls upgrade, ask a few practical questions.
What problem are we actually trying to solve?
Is the issue downtime, obsolete controls, poor data visibility, safety concerns, inconsistent quality, or something else?
Can the existing equipment be modernized?
Full replacement may not be necessary. A controls upgrade could potentially provide many of the required improvements.
How will the new system interact with existing equipment?
Integration planning is particularly important when old and new technologies need to coexist.
What information do operators need?
A technically impressive system isn’t very useful if operators can’t quickly understand what the HMI is telling them.
What happens after commissioning?
Ask about documentation, training, troubleshooting support, system maintenance, and future modifications.
How will safety be addressed?
Safety should be considered from the beginning of the project rather than treated as an afterthought.
Frequently Asked Questions
What are machine safety services?
Machine safety services help businesses identify machinery hazards and implement engineering controls and safety systems designed to reduce risk. They can include risk assessments, safety circuits, guarding evaluations, safety PLCs, interlocks, and validation.
What is control system integration?
Control system integration is the process of connecting automation hardware, software, machines, sensors, networks, and other technologies so they operate as a coordinated system.
Why modernize a legacy control system?
Legacy controls can become difficult to support, troubleshoot, or connect with modern technologies. Modernization can improve reliability, diagnostics, safety integration, data visibility, and maintainability while potentially extending the life of existing equipment.
Does automation improve machine safety?
Automation can support machine safety by integrating safety devices, monitoring hazardous conditions, and providing controlled responses. The appropriate solution depends on the specific machine, hazards, and risk assessment.
Can an integrator work with existing equipment?
Yes. Control system integrators often work with existing machinery and legacy controls. Depending on the equipment and project goals, modernization may involve replacing selected control components while retaining useful mechanical systems.
What industries use control system integration?
Control system integration is used across many sectors, including manufacturing, food and beverage, life sciences, transportation, entertainment, energy, and other industrial environments.
How can automation improve product quality?
Automation can reduce process variation by controlling equipment and process parameters consistently. Better monitoring and data collection can also help identify deviations earlier.
Final Thoughts
Industrial automation isn’t simply a race toward newer technology.
The real objective is more practical: safer equipment, dependable processes, useful information, and systems that make sense for the people who operate and maintain them.
That’s why machine safety services and control system integration should be considered together when businesses modernize industrial operations. A control system that runs efficiently but provides poor safety or visibility isn’t a complete solution.
Likewise, adding safety equipment without considering how the overall automation architecture works can leave valuable opportunities on the table.
Companies such as Pacific Blue Engineering demonstrate how systems engineering and automation technologies can be brought together to address those challenges across different industrial environments.
The next step for a facility considering modernization is often surprisingly simple: identify the machines, processes, or controls causing the most friction today. From there, a properly scoped engineering assessment can reveal what should be upgraded, what can stay, and where automation can deliver the greatest practical value.
-
 Education2 years ago
Mastering Excel: Your Comprehensive Guide To Spreadsheets And Data Analysis
-
 Tech2 years ago
How To Choose The Best Forex Trading Broker?
-
 Business2 years ago
Exploring the Rental Market: Properties for Rent in Malta
-

 Blog2 years ago
Arab MMA Fighters Shine Bright: Meet the Champions of PFL MENA
-

 Tech2 years ago
The Role Of Experts VS Top Mobile Apps for Green Screen Removal
-
 Travel2 years ago
Experience the Best Desert Safari Dubai Offers!
-
 Home Improvement3 years ago
Eco-Friendly Round Rug Options for Sustainable Living in NZ
-

 Tech2 years ago
Finding Unique Products and Deals on Social Media Marketplaces