
Tech
Navigating the World of IC Chips: A Guide for Electronics Manufacturers and Innovators

Integrated Circuits (IC Chips) stand out as the heartbeat of ultramodern technology in the rapidly evolving landscape of electronics manufacturing. These tiny electronic components have revolutionized living, working, and playing.
From smartphones to satellites, IC chips are integral to the functionality of nearly all electronic devices. This blog post aims to illuminate the significance of IC chips in electronics manufacturing, the current request dynamics, and how to choose the right IC chip supplier for your requirements.
What is an IC Chips?
IC chips, or integrated circuits, are more than just components; they are the heart of modern electronics. These tiny silicon chips host thousands to millions of transistors, making it possible to create smaller, faster, and more reliable devices than ever before. Their significance cannot be overstated, as they enable the development and miniaturization of technology.
Evolution of IC Technology
Significant milestones have marked the evolution of IC technology from analog to digital. Analog ICs, which process nonstop signals, laid the root of the electronics smash by enabling the miniaturization of radios, boxes, and early computers.
The arrival of digital ICs, which handle separate signals, further accelerated progress, paving the way for the development of complex computing systems, mobile dispatches, and the Internet. We stand on the cusp of a new period, with developments in computing and nanotechnology promising to review what’s possible with IC chips.
Sourcing IC Chips: A Guide for Electronics Manufacturers and Innovators
As the demand for IC chips grows, sourcing them has become a critical aspect of electronics manufacturing and innovation. With numerous suppliers and distributors, it is essential to understand factors such as quality, reliability, and cost when selecting IC chips.
Considerations like lead times, minimal order amounts, and packaging options must also be considered. Partnering with reputable suppliers and distributors is critical to ensuring a steady supply of high-quality IC chips for your electronic products.
Types of IC Chips Based on Packaging
The packaging of IC chips is an essential factor to consider when selecting the right type for a specific application. Different packaging options offer varying protection, performance, and cost-effectiveness. There are some types of integrated circuits based on packaging:
Dual In-Line Package (DIP):
This was one of the foremost forms of IC packaging, consisting of two rows of pins on the opposite sides of the chip. DIPs are generally low-cost and easy to use but take up more space than other packaging options.
Small Outline Integrated Circuit (SOIC):
SOIC chips have a smaller footprint than DIPs, making them popular in applications where space is limited. They have similar pin layouts as DIPs but with thinner leads for better heat dissipation.
Ball Grid Array (BGA):
In BGA packaging, the chip is mounted on a small ceramic or plastic board with an array of solder balls at its bottom. This type of packaging offers better thermal and electrical performance but may bear further work to assemble.
Chip Scale Package (CSP): CSPs are similar to BGAs, but the solder balls are placed directly under the chip, making them even smaller. They offer better performance and space-saving capabilities but require precise manufacturing techniques.
Quad Flat Package (QFP): QFPs have a square or rectangular shape with leads on all four sides of the chip. They provide good electrical performance and are commonly used in microcontrollers and digital signal processors.
Different Types of IC Chips Based on the Number of Transistors
The number of transistors in an IC chip is also a defining factor, with the following types of ICs based on their transistor count:
Small-scale integration (SSI): These chips have up to 100 transistors and are typically used for simple logic functions.
Medium-scale integration (MSI): MSI chips have between 100 and 3,000 transistors, enabling more complex functions like counters and decoders.
Large-scale integration (LSI): LSI chips have between 3,000 and 100,000 transistors, allowing for even more complex functions like microprocessors.
Very-large-scale integration (VLSI): VLSI chips can contain over 100,000 transistors and are used in advanced devices like computers and smartphones.
We can expect even more miniaturization and increased transistor counts in future IC chips as technology advances.
Popular Types of IC Chips
Some IC chips are more generally used than others due to their versatile nature and wide applications. These include:

Microprocessors: These ICs contain the processing unit of a computer or other electronic device, making them essential for calculating and controlling systems. They generally contain millions of transistors and offer high-speed performance.
Memory: Memory ICs store data in electronic devices. Exemplification include dynamic random access memory (DRAM), static random access memory (SRAM), and flash memory. The capacity and speed of these IC chips vary depending on the specific application.
Operational amplifiers (op-amps): Op-amps are versatile integrated circuits in various analog applications. They can amplify signals, perform mathematical operations, and act as filters or comparators. Their precise inputs and outputs make them crucial components in electronic circuits.
What is the difference between 2DIC and 3DIC?
2DICs are the most generally used type of IC and are typically manufactured on a single subcast or airplane. They consist of multiple electronic factors, such as transistors, resistors, and capacitors, connected on a flat face using essence traces. This type of IC is generally used in electronic devices such as smartphones, laptops, and other consumer electronics.
On the other hand, 3DICs are erected by vertically mounding multiple layers of circuitry on top of each other, creating a three-dimensional structure. This allows further factors to be packed into a lower space, making 3DICs more influential and vital than their 2DIC counterparts. Also, this structure allows for better heat dispersion, performing in bettered performance and trustability.
The manufacturing process for 3DICs is more complex and precious than that of 2DICs. It requires technical equipment and ways to fabricate the multiple layers and ensure precise alignment and connections between them. Still, 3DICs offer numerous benefits, such as reduced power consumption, increased speed, and better functionality.
Tips for Electronics Manufacturers in Choosing the Right IC Chips Supplier
When choosing the right IC chip supplier, there are a few key factors to consider.
Online Search
Utilizing search engines with specific keywords such as “Electronics Manufacturing,” “Sourcing IC Components,” and “IC Chips Supplier” can yield a plethora of options. However, the key is to look beyond the first page of search results.
Explore industry forums, read articles, and participate in discussions to gather insights and recommendations from peers in the electronics manufacturing and hardware development sectors.
.Company Certification
Company certifications should be among your top considerations when narrowing down your list of implicit suppliers. Certifications similar to ISO 9001 for quality operation systems or specific industry norms applicable to electronics manufacturing can indicate a supplier’s commitment to quality and nonsupervisory complaints.
These certifications ensure the supplier adheres to recognized best practices and standards in producing and testing IC chips.
Visit the Supplier Company
Still, visit the supplier’s manufacturing installation. This step offers an invaluable opportunity to assess the supplier’s operations firsthand. You will gain perceptivity into their manufacturing processes, quality control measures, and technological capabilities. A visit can also help you gauge their operations’ scale and ability to meet your supply demands.
Product Quality
Assess the quality of the consummated IC chips. Request samples for testing to ensure they meet your design’s specialized specifications and performance conditions. Pay attention to chip life, power effectiveness, and comity, among other components. High-quality IC chips can enhance your electronic devices’s overall continuity and functionality.
Supply Chain Transparency
In today’s global market, understanding the intricacies of your supplier’s supply chain is crucial. A transparent supply chain can help you anticipate potential delays or disruptions. Inquire about the supplier’s sourcing practices, inventory management, and lead times. Suppliers offering clear, detailed information about their supply chain practices will likely be more reliable.
Customer Feedback
Seek out feedback from current or former guests of the IC chips supplier. Client reviews, testimonials, and case studies can give precious insight into the supplier’s trustability, client service quality, and post-sales support. Pay special attention to commentary regarding how the supplier handles issues and resolves challenges.
Risk Management
In the volatile world of electronics manufacturing, the ability to manage and mitigate risks is essential. Discuss with potential suppliers their strategies for dealing with unexpected challenges, such as component shortages or geopolitical tensions that could impact supply chains.
A robust risk management plan indicates a supplier’s preparedness to ensure a steady supply under adverse conditions.
How do you program IC Chips?
Programming IC chips involves software and hardware tools to write the necessary code onto the chip’s memory. The process typically involves the following steps:
1. Design and test the code: Before programming, you must design and test your code on a computer or other device.
2. Prepare the programming tool: Depending on the type of IC chip, you may need specific hardware tools, such as a programmer or emulator, to transfer the code onto the chip’s memory.
3. Connect the tool to the IC chip: Follow the manufacturer’s instructions on connecting the programming tool to your specific IC chip.
4. Transfer the code: Use the programming software to transfer your code onto the IC chip’s memory once connected.
5. Verify and test: After programming, verifying that the code has been successfully written onto the chip is crucial. You can do this by running tests on the IC chip or connecting it to a device and ensuring it functions as intended.
6. Repeat if necessary: If any issues arise, you may need to repeat the programming process until your code is successfully transferred and functioning correctly on the IC chip.
Challenges and Future Trends
Despite the exciting potential of IC chips, the industry faces several challenges. The ever-increasing demand for higher performance and lower costs can strain manufacturers’ capabilities, while the shrinking size of IC chips poses new technical difficulties.
Industry players are exploring new materials, processes, and design methodologies to advance IC technology further. Some promising trends include 3D ICs, heterogeneous integration, and new materials like graphene. The future looks bright for IC chips as innovations continue to push the boundaries of what is possible.
Conclusion
Understanding and leveraging the potential of IC chips is essential for success in today’s competitive landscape for electronics manufacturers, hardware developers, and innovators. Selecting the right IC chips supplier is a strategic decision that can influence your electronics manufacturing projects’ quality, cost, and success.
By keeping abreast of technological advancements, building strategic partnerships with suppliers, and investing in research and development, stakeholders can navigate the complexities of the IC chip world and shape the future of electronics.
FAQS
What is the main feature of IC?
The main feature of Integrated Circuits (ICs) is their ability to pack many electronic components onto a single chip. This miniaturization allows for smaller, more powerful devices, making ICs essential in modern electronics technology.
What are the applications of IC?
ICs have various applications in various fields, such as telecommunications, consumer electronics, medical devices, the automotive industry, aerospace and defense, and many more. They are used in almost every electronic device, from smartphones and computers to household appliances and transportation systems.
What is the purpose of IC programming?
IC programming aims to design and implement the instructions and functions that control the behavior of an integrated circuit. This programming involves writing code using specific programming languages, such as Verilog or VHDL, which are then converted into a physical layout on the chip through synthesis.
What is the most crucial advantage of an IC?
This miniaturization also leads to lower power consumption, faster operation speeds, and reduced production costs. It allows for creation of smaller and more powerful electronic devices, revolutionizing how we communicate, work, and live. ICs also offer improved performance and reliability compared to discrete circuits since they have fewer external connections that can fail or cause interference.
Why is it important to choose the right distributor?
Choosing the right distributor is crucial in ensuring that ICs are high quality and meet the required specifications. Distributors act as a bridge between manufacturers and end-users, providing access to various ICs for various applications.
Since January 1, 2026, structured electronic invoicing has become mandatory for almost all transactions between Belgian VAT-registered businesses. These invoices are exchanged through the Peppol network instead of with traditional PDF-based processes. For businesses, the decision on the provider can have a lot to do with what’s the destination of the invoice than it does with the transaction itself. Integration, inbound processing, validation, monitoring, security, and support can all be key factors to how well e-Invoicing integrates into everyday finance operations. An easy way to evaluate a Peppol access point Belgium solution is to see what happens before, during, and after an invoice moves through the network.
- ERP and accounting integration.
The first question would be how well the Access Point is integrated into the existing systems used by the business. An enterprise can generate invoices from an ERP, billing application, or multiple systems of different subsidiaries in different companies. The Access Point needs to have the invoice information without creating an extra manual process for each system and how that invoice data needs to be sent to the Access Point. This means not just a simple integration statement. Businesses should know which APIs, connectors, and formats are available and how data is mapped and whether invoice status can be sent back to the ERP. In a large organization, the integration model should also be flexible for future change. Another legal entity or ERP should not need to be added to the overall e-Invoicing system.
- Stronger support for Sending and receiving.
A common mistake is to evaluate a provider on outbound invoicing. Belgian businesses need to be able to receive structured electronic invoices from their suppliers. Businesses should adapt their systems to receive structured invoices, for example, those that mainly invoice private individuals, the Belgian authorities say.
So, both directions should benefit from the Access Point. For incoming invoices, companies should assess where documents are led in accounting or ERP, whether supplier information can be matched automatically, and how exceptions are handled if an invoice can’t be processed.
- Invoice Validations before the Invoice Is Processed in the Network.
An efficient Access Point cannot be thought of as just a delivery mechanism. Data on the invoice needs to be structured according to the proper business and structure and business rules in order to be processed properly. Validation makes it possible to identify missing and inaccurate data before the invoice is sent.
This is particularly useful for the organizations that receive their invoices from different sources. If data is created using different systems, validation is most important so that there are no mistakes. The vendor should be able to provide an explanation of the types of validations in place, the location of those validations, and the outcome of those validations that are not successful.
- Visibility Into Invoice Status and Exceptions.
Once an invoice has been sent, finance teams need to know what happened to it. A Belgium e-invoicing solution should have clear visibility into transaction status, delivery, and errors in Belgium. Ideally, this information should flow back into the enterprise’s current finance workflow rather than being stuffed away in a provider dashboard. Particularly when invoice volumes are high. A finance team should be able to determine which invoices got processed and which ones should be paid attention to and why the transaction failed at the end of the month. Searching, filtering, and reporting on these events can also facilitate month-end reconciliation as well.
- Scalability across entities and Invoice volumes.
An Access Point that works for one legal entity may not necessarily be appropriate for a multinational with multiple Belgian entities. Enterprises should look into transaction volumes, number of entities, ERP environment, and suppliers and customer relationships before choosing a provider. They should know how onboarding works when a new entity enters the network. Will it also need an implementation in a new system? Can multiple entities be managed centrally? How do Peppol identifiers get handled? These questions help to determine whether a Belgium Peppol Access Point can be part of the organization’s operating model and not just its invoice volume.
- Provider Support and Long-Term Operations.
What happens after implementation is the last step. A certified Peppol provider Belgium should be able to support the enterprise when integrations change, transaction failures occur, or new requirements impact the invoicing process. Before the contract is signed, the support arrangements should be in place. Enterprises should know the response time, escalation procedure, maintenance window, and responsibilities if there is an ERP, Access Point, or recipient issue. It is also worth checking if the provider can support monitoring and reporting without having finance teams lean on technical experts completely.
What Should Enterprises consider When Comparing?
Enterprises should not just choose providers based on network connectivity alone and compare them in terms of their network compatibility. They may rather compare on the following points: • Integration with ERP and accounting
• Sending and receiving features
• Invoice verification
• Status and exceptions handling
• Multi-company
• Security and business continuity
• Support and service management.
A company with one accounting system and few invoices may prefer something less complicated. An enterprise with multiple ERP systems will generally need more sophisticated integration and monitoring.
The Belgian authorities are careful to distinguish between end-user software and service providers providing the services to Peppol. Companies that have this software and can choose their own Access Point are referred to as certified service providers.
The Right Access Point Should Fit the Entire Invoice Process.
The purpose in choosing a Belgium e-Invoicing service provider was not to connect the company with Peppol. The service provider will be a part of the whole system through which invoices have to be sent, received, and tracked.
So Peppol Belgium readiness is as much an operational issue as it is a compliance issue. The company could put even more pressure on Finance if the service provider is a good partner for connectivity but not good at tracking failure. To the contrary, a solution that works well with one ERP but does not work well for multi-entity processes will soon start to look restrictive as the business grows.
So for an enterprise that is considering Peppol access point Belgium service, the right assessment always starts with the invoice process. How is the invoice created? How is it sent to the Access Point? Are there any validations prior to sending it out? How is it received by the recipient? What happens in case of failure? Can Finance trace the problem without having to follow another manual process? These considerations will help us choose an Access Point for enterprise e-Invoicing that works well.
Best Managed IT Services Companies for Proactive IT Support
IT issues don’t usually come up at an opportune time either; the failure of servers, security threats, or network slowdowns can disrupt business operations and cause delays that can end up being costly. That is why a number of companies turn to managed IT services with their emphasis on prevention rather than reaction.
The best managed IT service providers have all of the following capabilities: monitoring, automation, cybersecurity, maintenance, and technical skills. In addition, the proper provider is able to tailor its preventative strategy to fit the size of the company.
Best Managed IT Services Companies for Proactive Support
For firms considering IT management services, a more proactive approach is required than just basic help desk services. Proactive service involves monitoring systems and taking care of issues even before they turn into major problems.
1. Longi Engineering
Longi Enginuity Technologies is a strong choice for businesses seeking proactive managed IT support. Its approach focuses on maintaining reliable technology through continuous oversight, cybersecurity, technical support, and preventive IT management.
Proactive managed services ensure that any technical issues are detected prior to creating any disruptions. The process includes maintenance, security, and troubleshooting of the network to prevent any downtime.
2. IBM Managed Services
IBM Managed Services is highly suitable for large organizations with highly complicated IT setups. These include its strong points, such as hybrid cloud management, artificial intelligence, and IT operations at the enterprise level.
One of the greatest benefits is the analysis of infrastructure information by means of AIOps, which helps recognize possible problems that could affect the performance of IT infrastructures.
3. Accenture Managed Services
Accenture offers managed IT services along with cloud management, digital transformation, and cybersecurity. This comprehensive service offering makes Accenture a suitable choice for firms that deal with a complex IT landscape.
A proactive strategy offered by Accenture includes infrastructure monitoring, security analysis, and compliance management. This will help companies to uncover any potential problems that may affect their operations.
4. HCLTech
HCLTech offers managed infrastructure services, service desk support, automation, and hybrid workplace management. Its approach is particularly relevant for organizations that want routine IT tasks handled consistently.
The DRYiCE automation solution can facilitate automated maintenance and automated incident management. These processes will reduce the need for manual effort while resolving all the problems even before they arise.
5. Tata Consultancy Services
Tata Consultancy Services provides managed infrastructure and cloud services for large organizations operating at significant scale. Its services emphasize automation, monitoring, and efficient enterprise IT management.
TCS uses its Ignio AIOps platform to detect unusual system behavior and identify potential issues. Its automation capabilities can also support faster resolution and more consistent infrastructure performance.
Strong Managed IT Providers for Growing Businesses
Enterprise providers are not the only options for proactive IT support. Mid-market and growing businesses often need providers that combine continuous monitoring with responsive service, security, and practical IT management. Managed IT Services Connecticut represents this type of ongoing support, where businesses can rely on managed technology oversight instead of handling every IT issue internally.
6. Ntiva
Ntiva provides managed IT services, cybersecurity, compliance, and IT strategy. The company’s solutions are suitable for firms that require consistent supervision while not keeping all IT services within their walls.
Continuous monitoring helps in identifying technical and security issues early on. Also, because it is compliance-based, it is an ideal choice for firms that have to abide by certain regulatory standards.
7. Dataprise
Dataprise provides managed IT, cloud, infrastructure, and cybersecurity services for mid-market firms. The approach entails ensuring there is visibility within the technological environment of the business and finding any weaknesses that may exist.
Network assessment and threat hunting help in the proactive management of risks. Through this service, businesses will be able to manage any infrastructure or cybersecurity challenges proactively.
8. Thrive
Thrive provides managed IT services with a focus on cloud environments, cybersecurity, infrastructure, and digital transformation. Its services are suited to growing businesses managing increasingly complex technology systems.
Continuous application and network monitoring can help identify performance concerns early. Its hybrid cloud capabilities also support organizations moving between traditional infrastructure and cloud-based environments.
What Makes a Managed IT Provider Proactive?
The choice of a managed IT services company is not just about the comparison of its services. A true proactive vendor has an infrastructure set up in such a way that any issues can be detected and solved before downtime occurs. Connecticut managed IT services adhere to this philosophy by concentrating on management and not on technical problems.
Continuous Monitoring
A good provider will continuously monitor their networks, servers, endpoints, applications, and other systems. Notifications allow their technical staff to investigate any suspicious behavior and prevent it from becoming a bigger problem.
Automated Maintenance
Regular patching, updates, system checks, and routine maintenance reduce preventable technology problems. Automation helps these tasks happen consistently without depending entirely on manual intervention.
Integrated Cybersecurity
Preventive IT support is also crucial to handling security threats. Threat management, endpoint security, vulnerability management, and access control all play a role in minimizing the risk of turning a security threat into a breach.
Predictive IT Management
Sophisticated service providers employ analytical tools and automation to uncover trends that point towards future failure. Through this, IT departments can take action based on trends rather than user complaints.
Choosing the Right Provider for Proactive IT Support
The appropriate provider will be determined by the technology environment within the organization, the size of the organization, its security needs, and its business objectives. In some cases, the large corporation may need a provider that has hybrid cloud capabilities along with automation capabilities, whereas other organizations may need only a focused managed service partner.
Another criterion that an organization must consider when selecting an appropriate provider is that of processes and measurable performance standards for service delivery.
Building a More Proactive IT Environment
Proactive IT support is ultimately about preventing avoidable disruption. The strongest managed IT services companies continuously monitor technology, automate routine maintenance, strengthen security, and use data to identify emerging problems.
Selecting a provider with these capabilities creates a more structured approach to IT management. Longi Enginuity Technologies can support this proactive model through managed IT services designed around business technology needs. The right partnership helps turn IT from a source of unexpected problems into a stable foundation for daily operations.
Tech
Machine Safety Services and Control System Integration: Building Safer, Smarter Industrial Operations

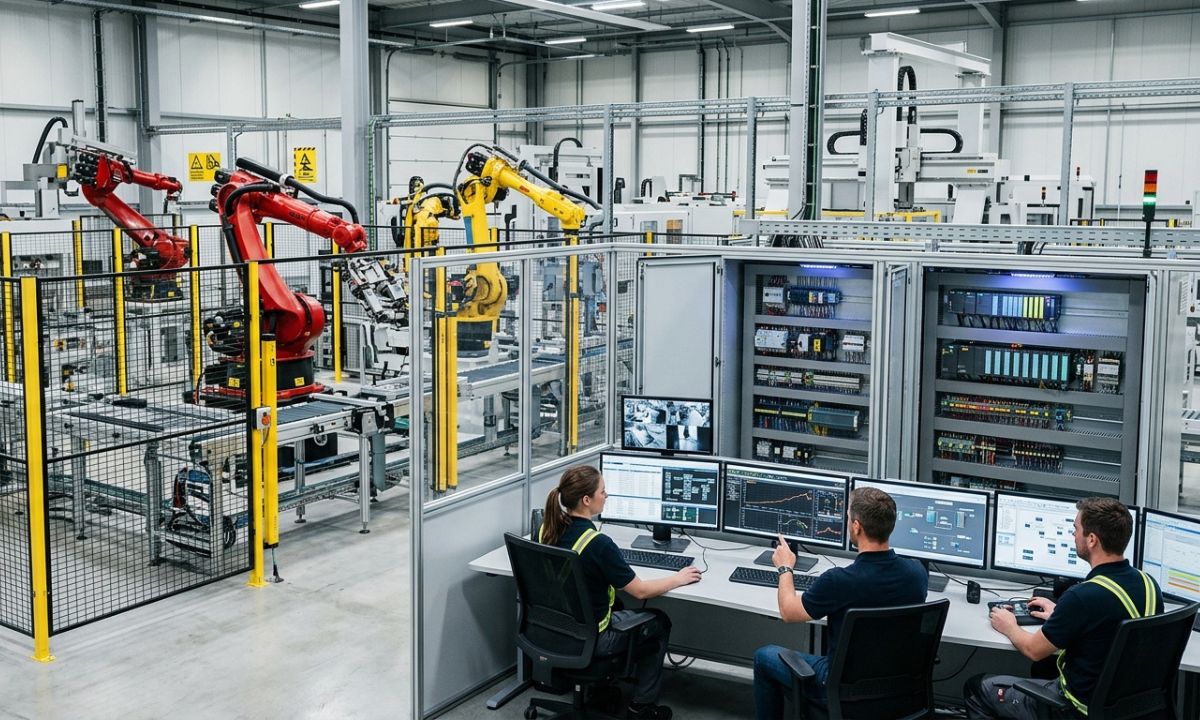
A production line can run thousands of cycles in a day without a problem. Then one small control failure, an outdated safety circuit, or a poorly integrated machine creates a serious interruption.
That is why modern industrial automation is no longer just about making equipment run faster. It is about making systems work together safely, reliably, and intelligently.
This is where machine safety services and control system integration become particularly important. Manufacturers and other industrial operators need more than individual machines with sophisticated controls. They need those machines, safety devices, sensors, software, and production systems to communicate effectively.
A well-designed automation system can improve productivity while also helping reduce operational risk, improve product consistency, modernize aging equipment, and give plant managers better visibility into what is happening on the production floor.
For companies dealing with legacy controls or increasingly complex production requirements, that combination can make a substantial difference.
Table of Contents
- What Are Machine Safety Services?
- Understanding Control System Integration
- Why Machine Safety and Automation Go Together
- Common Problems With Legacy Control Systems
- What a Control System Integrator Actually Does
- Key Benefits of Modern Automation Integration
- Machine Safety Services vs. Traditional Safety Upgrades
- How Pacific Blue Engineering Supports Industrial Automation
- Industries That Can Benefit From Control Integration
- Questions to Ask Before Starting an Automation Project
- Frequently Asked Questions
- Final Thoughts
What Are Machine Safety Services?
Machine safety services are engineering and technical services designed to identify and reduce hazards associated with industrial machinery and automated processes.
These services can involve reviewing existing equipment, identifying potential hazards, evaluating safety controls, and helping businesses implement appropriate protective measures.
Depending on the application, machine safety work may include:
- Safety risk assessments
- Machine guarding evaluation
- Safety circuit design
- Emergency stop systems
- Safety PLC implementation
- Interlocking systems
- Presence sensing devices
- Light curtains and safety scanners
- Safety relay systems
- Control system validation
- Safety documentation
- Machine modernization
The important point is that machine safety isn’t simply about adding an emergency-stop button and calling the job finished.
A machine may be technically functional while still having weaknesses in its safety architecture. For example, an outdated control panel may not communicate properly with newer safety devices. A modified production line may introduce hazards that weren’t present when the original machine was installed.
That’s why safety needs to be considered as part of the complete automation system.
Understanding Control System Integration
Control system integration involves bringing different automation components together so they operate as one coordinated system.
Think about a modern production facility. It may contain programmable logic controllers, variable frequency drives, robots, sensors, HMIs, industrial networks, safety systems, databases, and supervisory software.
If each component works independently, operators may spend unnecessary time troubleshooting problems and collecting information manually.
An experienced control system integrator connects these technologies and develops the control architecture needed for the application.
A typical integration project might include:
- Reviewing the existing process
- Identifying operational requirements
- Developing the control architecture
- Selecting suitable automation hardware
- Programming PLCs and HMIs
- Integrating sensors and field devices
- Connecting safety systems
- Establishing industrial communications
- Testing the system
- Commissioning the equipment
- Training operators and maintenance personnel
The goal isn’t simply to install new technology. The goal is to create a system that solves an actual operational problem.
Why Machine Safety and Automation Go Together
Safety and productivity are sometimes treated as separate objectives. In practice, they often overlap.
Consider a machine that frequently stops because operators have to manually intervene. If the safety and control architecture is poorly designed, diagnosing those stops can become difficult.
A modern integrated system can provide clearer information about what happened and why.
For instance, instead of simply showing that a machine stopped, an HMI might identify a particular safety device, interlock, sensor, or process condition that triggered the shutdown.
That information can shorten troubleshooting time.
It can also help maintenance teams identify recurring issues before they turn into larger production problems.
Honestly, this isn’t talked about enough: good safety engineering can contribute to better operational visibility, not just compliance.
Common Problems With Legacy Control Systems
Many industrial facilities are still operating equipment that was installed years or even decades ago.
There’s nothing inherently wrong with keeping reliable equipment in service. The problem begins when the control technology becomes difficult to maintain or integrate.
Common warning signs include:
Obsolete PLC Hardware
Older PLCs and processors may no longer be supported by their manufacturers. Replacement components can become expensive or difficult to locate.
Limited Data Visibility
Some older systems provide very little useful production data. Operators may know that something went wrong but have limited information about the cause.
Difficult Troubleshooting
Legacy systems may rely heavily on undocumented wiring, outdated programming practices, or components that newer technicians aren’t familiar with.
Inconsistent Safety Architecture
Equipment modifications performed over the years can leave safety systems fragmented or difficult to evaluate as a whole.
Poor Communication Between Machines
Older equipment may not communicate easily with modern manufacturing software, plant networks, or newer automation platforms.
Replacing an entire machine isn’t always the answer.
In many situations, control system modernization can extend the useful life of existing equipment while bringing its controls closer to modern operational standards.
What a Control System Integrator Actually Does
A control system integrator sits between the business problem and the technology used to solve it.
That distinction matters.
A good integrator doesn’t start with, “Which PLC should we install?” The better question is, “What does this process need to accomplish?”
From there, engineers can determine the appropriate hardware, software, networking, safety architecture, and user interface.
An experienced integrator may work on projects involving:
- PLC programming
- HMI development
- SCADA systems
- Industrial networking
- Robotics integration
- Motion control
- Variable frequency drives
- Safety PLCs
- Electrical control panels
- Data collection
- Process automation
- Legacy system modernization
- System commissioning
This approach becomes especially useful when a project involves multiple vendors or generations of equipment.
Someone has to make all those pieces work together.
Key Benefits of Modern Automation Integration
A properly planned automation project can affect much more than machine speed.
Improved Machine Safety
Modern safety systems can help identify hazards and provide controlled responses when unsafe conditions occur.
Better Product Quality
Automation can reduce process variation by controlling important parameters consistently.
Reduced Downtime
When control systems provide better diagnostic information, maintenance teams can often identify problems faster.
Lower Operational Risk
Replacing unsupported components and improving system architecture can reduce some risks associated with aging equipment.
Better Production Data
Integrated systems can collect valuable information about machine status, production rates, faults, energy use, and other operational factors.
Easier Maintenance
Clearer programming, documentation, interfaces, and diagnostics can make systems easier for maintenance teams to understand.
Longer Equipment Life
Modernizing controls may allow an otherwise useful machine to remain productive without replacing the entire mechanical system.
Better Decision-Making
Plant managers can make more informed decisions when reliable production information is available instead of relying entirely on manual observations.
Machine Safety Services vs. Traditional Safety Upgrades
| Traditional Approach | Integrated Machine Safety Approach |
|---|---|
| Focuses mainly on individual safety devices | Considers the complete machine and control architecture |
| Often reactive | Can be based on systematic risk assessment |
| Limited diagnostic information | Better fault and status visibility |
| May rely heavily on standalone components | Can integrate safety PLCs and control systems |
| May address one machine at a time | Can consider connected production processes |
| Documentation may be limited | Documentation and validation can be built into the project |
This doesn’t mean every facility needs the most sophisticated safety technology available.
Quite the opposite.
The right solution depends on the machine, process, hazards, operating environment, and business requirements.
How Pacific Blue Engineering Supports Industrial Automation
Pacific Blue Engineering is an example of an engineering company focused on control system integration and industrial automation.
Its work covers tailored automation solutions designed around the specific requirements of industrial operations rather than forcing every customer into the same technology package.
That distinction is important because no two production environments are exactly alike.
A manufacturing plant may need to modernize legacy controls while maintaining existing equipment. A food and beverage operation may have different process, sanitation, and production requirements. A life sciences facility can have its own demanding automation and documentation considerations.
Pacific Blue Engineering provides control system integration services across industries including manufacturing, food and beverage, life sciences, entertainment, and transportation.
Its engineering approach can help businesses address several common industrial challenges, including:
- Modernizing legacy control systems
- Improving machine safety
- Optimizing production processes
- Enhancing product quality
- Reducing operational risk
- Integrating automation technologies
- Improving access to operational information
The value of this type of engineering work isn’t limited to the initial installation.
A well-designed system should also make sense five or ten years later when someone needs to troubleshoot a sensor, modify a process, replace a component, or understand why a machine stopped.
That’s where thoughtful systems engineering earns its keep.
Industries That Can Benefit From Control Integration
Manufacturing
Manufacturers often need to balance throughput, quality, safety, and equipment availability. Integrated controls can help coordinate machines and provide better information about production performance.
Food and Beverage
Food and beverage facilities depend heavily on consistent processes. Automation can help control production parameters while improving visibility into equipment and process conditions.
Life Sciences
Life sciences operations can involve complex processes where consistency, traceability, and reliable automation are particularly important.
Entertainment
Entertainment facilities can use sophisticated automation and control systems for equipment, attractions, specialized machinery, and operational processes.
Transportation
Transportation environments may involve complex mechanical and electrical systems that require reliable monitoring, control, and integration.
The technologies differ between these industries, but the underlying principle remains similar: connect the right systems and make them work together reliably.
Questions to Ask Before Starting an Automation Project
Before selecting an integrator or beginning a major controls upgrade, ask a few practical questions.
What problem are we actually trying to solve?
Is the issue downtime, obsolete controls, poor data visibility, safety concerns, inconsistent quality, or something else?
Can the existing equipment be modernized?
Full replacement may not be necessary. A controls upgrade could potentially provide many of the required improvements.
How will the new system interact with existing equipment?
Integration planning is particularly important when old and new technologies need to coexist.
What information do operators need?
A technically impressive system isn’t very useful if operators can’t quickly understand what the HMI is telling them.
What happens after commissioning?
Ask about documentation, training, troubleshooting support, system maintenance, and future modifications.
How will safety be addressed?
Safety should be considered from the beginning of the project rather than treated as an afterthought.
Frequently Asked Questions
What are machine safety services?
Machine safety services help businesses identify machinery hazards and implement engineering controls and safety systems designed to reduce risk. They can include risk assessments, safety circuits, guarding evaluations, safety PLCs, interlocks, and validation.
What is control system integration?
Control system integration is the process of connecting automation hardware, software, machines, sensors, networks, and other technologies so they operate as a coordinated system.
Why modernize a legacy control system?
Legacy controls can become difficult to support, troubleshoot, or connect with modern technologies. Modernization can improve reliability, diagnostics, safety integration, data visibility, and maintainability while potentially extending the life of existing equipment.
Does automation improve machine safety?
Automation can support machine safety by integrating safety devices, monitoring hazardous conditions, and providing controlled responses. The appropriate solution depends on the specific machine, hazards, and risk assessment.
Can an integrator work with existing equipment?
Yes. Control system integrators often work with existing machinery and legacy controls. Depending on the equipment and project goals, modernization may involve replacing selected control components while retaining useful mechanical systems.
What industries use control system integration?
Control system integration is used across many sectors, including manufacturing, food and beverage, life sciences, transportation, entertainment, energy, and other industrial environments.
How can automation improve product quality?
Automation can reduce process variation by controlling equipment and process parameters consistently. Better monitoring and data collection can also help identify deviations earlier.
Final Thoughts
Industrial automation isn’t simply a race toward newer technology.
The real objective is more practical: safer equipment, dependable processes, useful information, and systems that make sense for the people who operate and maintain them.
That’s why machine safety services and control system integration should be considered together when businesses modernize industrial operations. A control system that runs efficiently but provides poor safety or visibility isn’t a complete solution.
Likewise, adding safety equipment without considering how the overall automation architecture works can leave valuable opportunities on the table.
Companies such as Pacific Blue Engineering demonstrate how systems engineering and automation technologies can be brought together to address those challenges across different industrial environments.
The next step for a facility considering modernization is often surprisingly simple: identify the machines, processes, or controls causing the most friction today. From there, a properly scoped engineering assessment can reveal what should be upgraded, what can stay, and where automation can deliver the greatest practical value.
-
 Education2 years ago
Mastering Excel: Your Comprehensive Guide To Spreadsheets And Data Analysis
-
 Tech2 years ago
How To Choose The Best Forex Trading Broker?
-
 Business2 years ago
Exploring the Rental Market: Properties for Rent in Malta
-

 Blog2 years ago
Arab MMA Fighters Shine Bright: Meet the Champions of PFL MENA
-

 Tech2 years ago
The Role Of Experts VS Top Mobile Apps for Green Screen Removal
-
 Travel2 years ago
Experience the Best Desert Safari Dubai Offers!
-
 Home Improvement3 years ago
Eco-Friendly Round Rug Options for Sustainable Living in NZ
-

 Tech2 years ago
Finding Unique Products and Deals on Social Media Marketplaces